Rolling Contact Fatigue (RCF): Origins, Identification, and Effective Grinding Mitigation Strategies
- Share
- Issue Time
- Apr 10,2026
Summary
Rolling Contact Fatigue is a critical defect impacting the safety and service life of railway infrastructure.
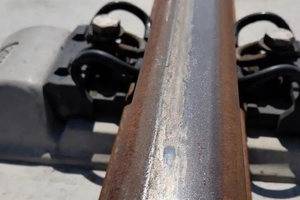
In modern high-speed and heavy-haul rail operations, immense contact stresses between wheel and rail are inevitable. When these cyclic stresses exceed the elastic limit of the rail steel, Rolling Contact Fatigue (RCF) initiates at or just below the rail surface.
RCF begins with microscopic plastic deformation and work hardening. Under repeated wheel passages, this leads to ratcheting—a cumulative plastic strain—which eventually causes fatigue cracks to form once the material's toughness limit is reached.
The progression of RCF is typically staged:
● Micro-cracks: Visible to the naked eye but without spalling.
● Minor Spalling Cracks: Slightly tactile, with minor localized spalling.
● Severe Spalling Cracks/Spalls: Characterized by significant crack depth and length, leading to large-scale material loss and potentially evolving into transverse defects, posing a severe safety risk.
Fish-scale spalling is prevalent on the gauge face of small-radius curves, while linear spalling is common on large-radius curves or tangent tracks. Unaddressed, RCF drastically shortens rail and turnout life, compromises ultrasonic inspection accuracy due to spalls, and in extreme cases, can lead to rail fractures.
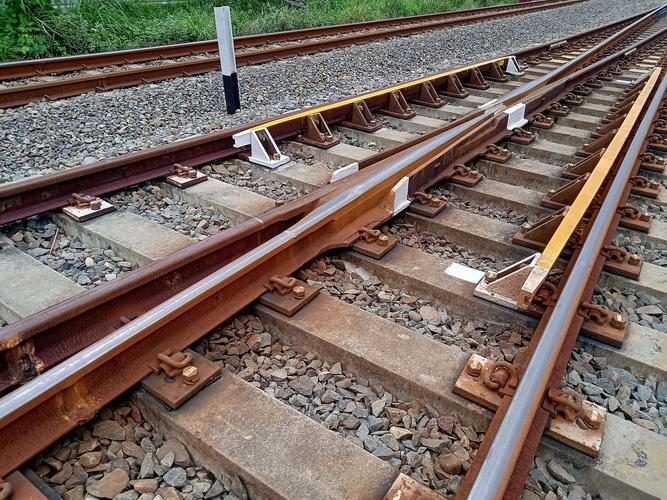
Effective RCF Management: Precision Rail Grinding is Key
The cornerstone of controlling and eliminating RCF is scientific and precise grinding.
● Preventive Grinding: The primary strategy to delay RCF initiation. By periodically removing an ultra-thin hardened layer (typically around 0.1mm), micro-defects are eliminated before cracks can form. This proactive "treat before it breaks" approach maintains track geometry and surface integrity at a lower lifecycle cost and forms the foundation of modern asset management.
● Corrective Grinding: Once RCF is detected, immediate grinding (or milling) is essential. For high-speed lines, the objective is the complete removal of all fatigue cracks; for conventional lines, all spalls must be fully removed. Corrective grinding demands greater metal removal rates and comprehensive angular coverage to ensure the entire network of initiated cracks is eradicated from the rail surface.
Grinding operations must adhere to specific angular coverage protocols: focus on the -10° to +20° range of the rail crown for tangents and low rails on curves; for high rails on curves, first restore the profile to its target geometry, followed by full coverage grinding from -10° to +45° to ensure thorough removal of fatigue damage.
The Interplay of Key Grinding Parameters
Effective RCF management relies not only on the right grinding strategy but also on the precise control of three interdependent process parameters: operating speed, downforce, and Material Removal Rate (MRR). These parameters collectively determine grinding quality and thermal input.
● Operating Speed dictates the efficiency of a single pass and track possession time. High-speed grinding (e.g., 60-80 km/h) improves productivity but reduces the dwell time per unit area, requiring wheels with superior sharpness and heat dissipation capabilities.
● Downforce directly influences the contact intensity and metal removal efficiency. Insufficient downforce fails to remove the hardened layer and cracks effectively, while excessive downforce can overheat the rail surface and induce new thermal damage.
● Material Removal Rate (MRR) is the core metric for grinding efficiency. For RCF remediation, MRR must be high enough to penetrate the crack depth; for preventive grinding, MRR is kept low (e.g., 50-150 mm³/s) to achieve a fine finish. Operators must dynamically adjust these three parameters based on RCF severity to balance grinding quality, operational efficiency, and rail substrate protection.
The RailwayCare Solution: Reliable Performance for Efficient Grinding Operations
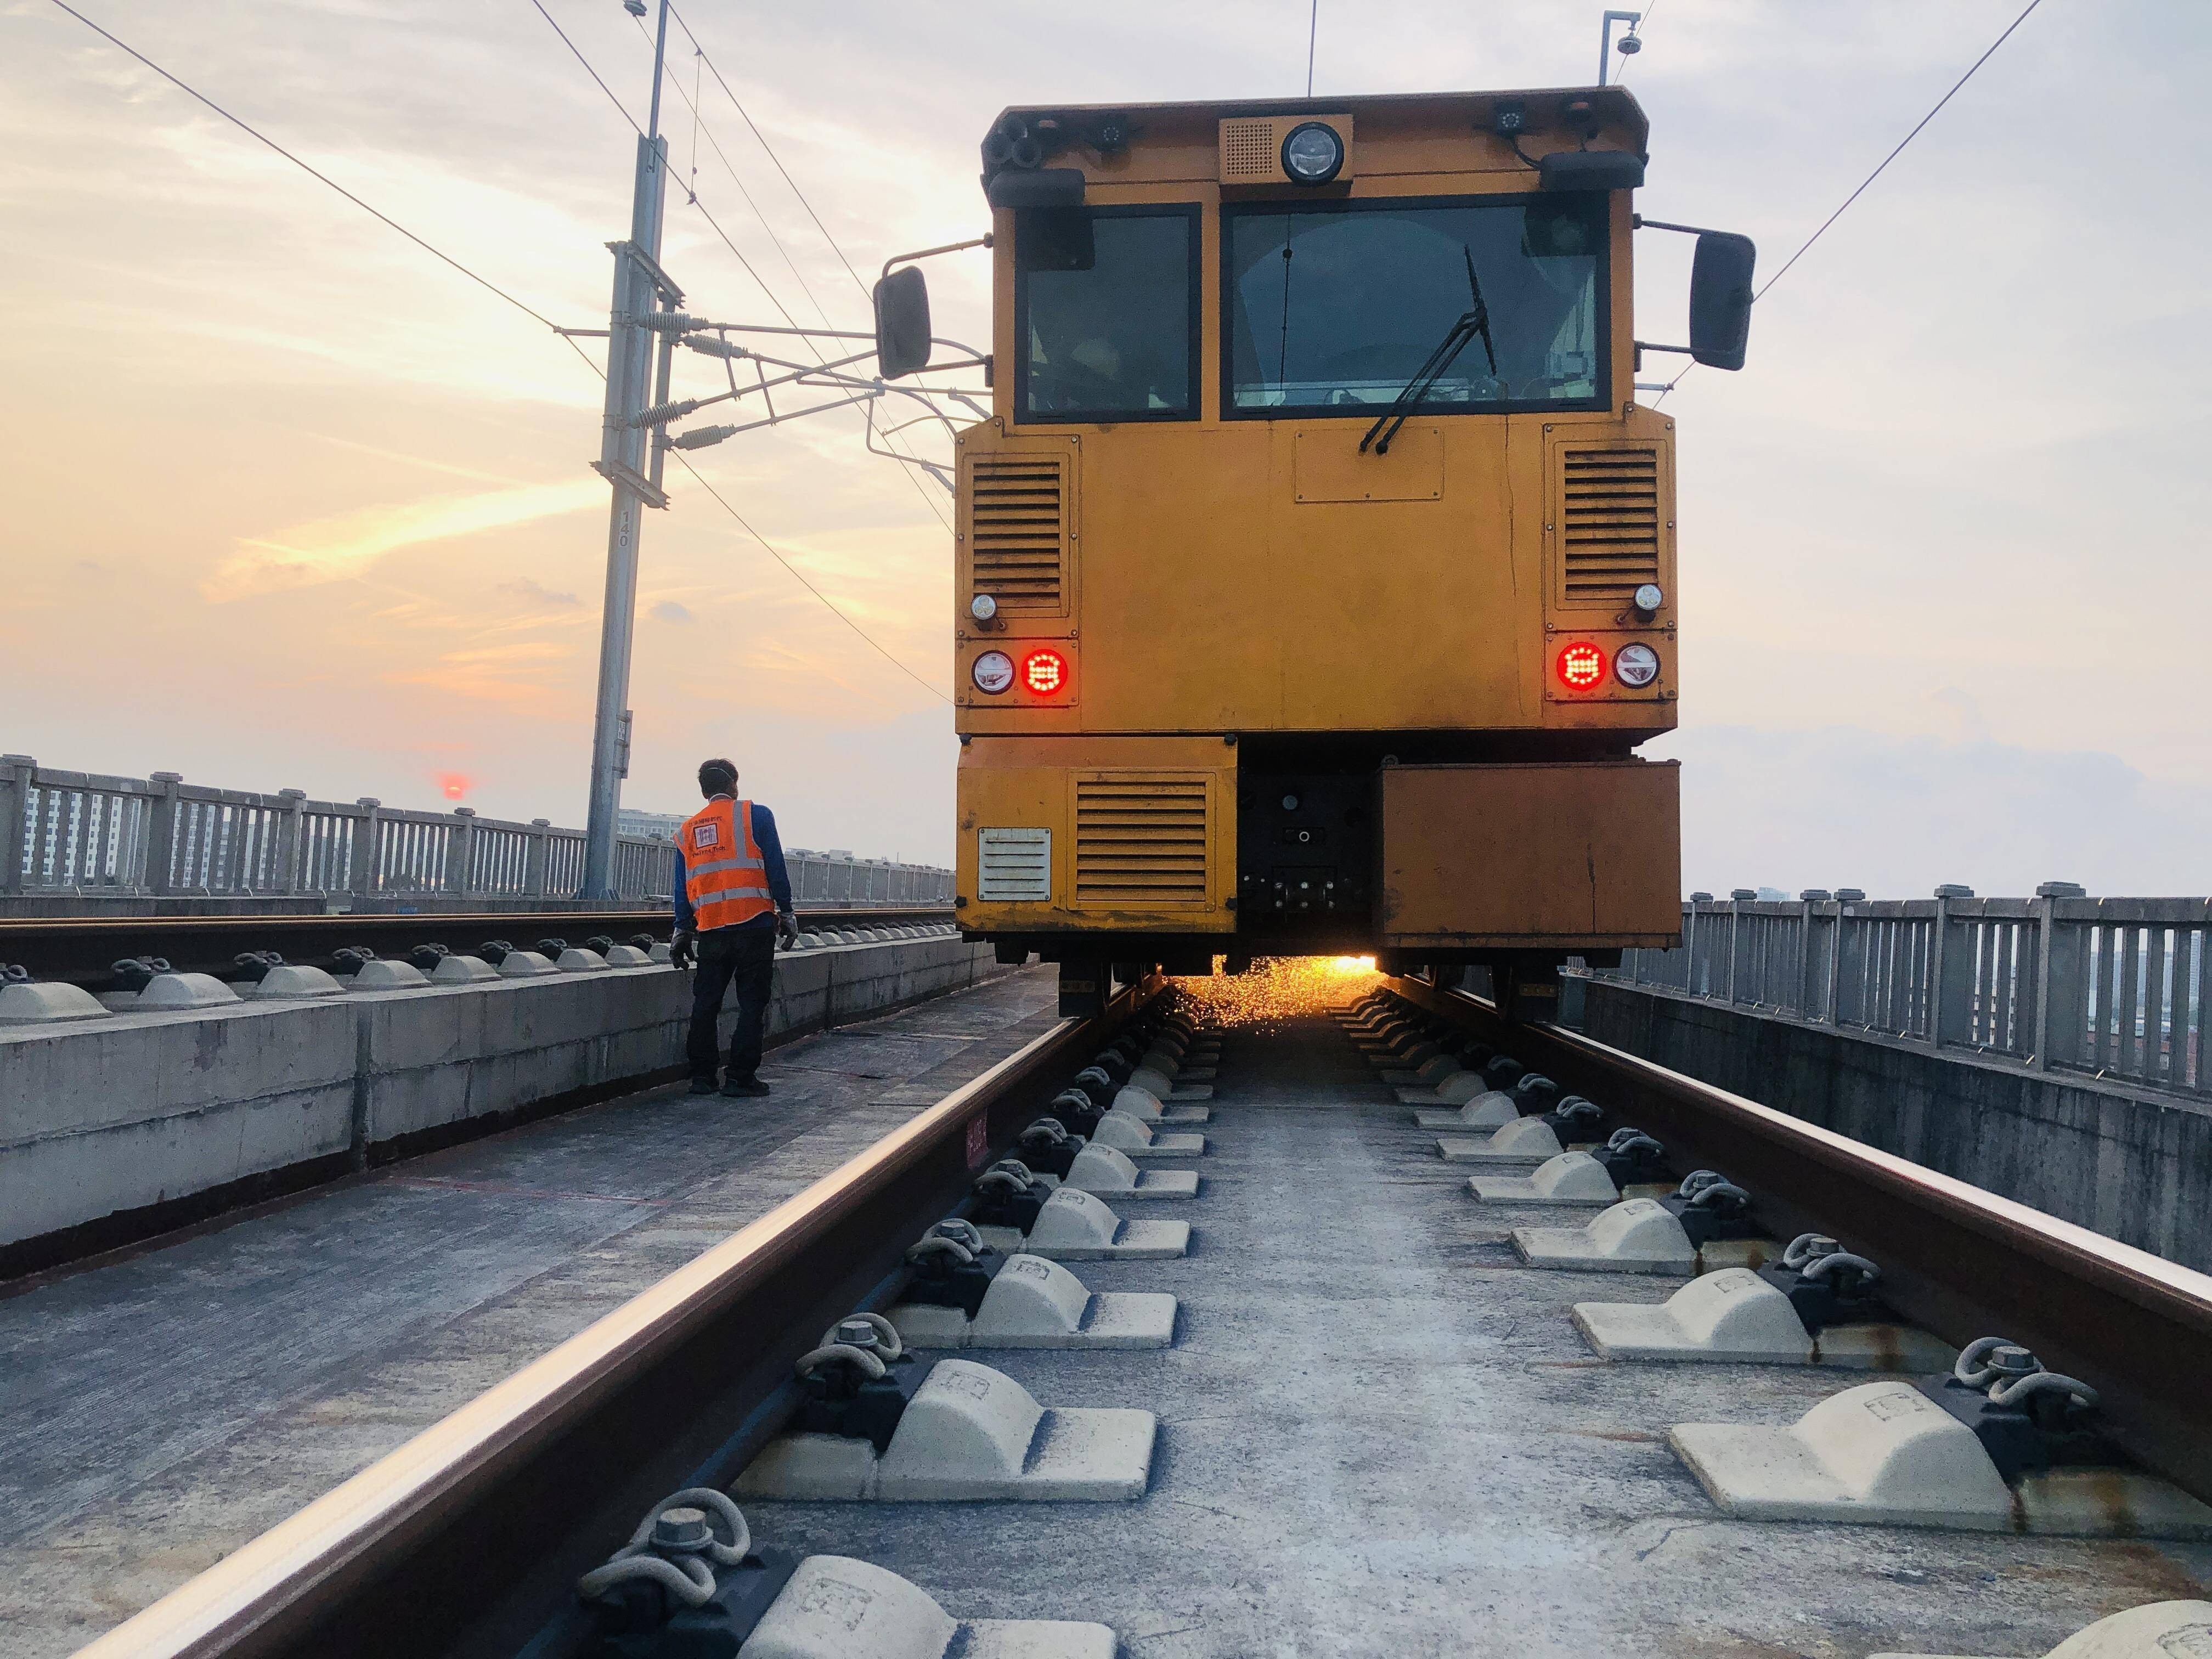
Addressing the demanding efficiency and precision requirements of RCF management, the Molaton RailwayCare range of grinding wheels offers a high-performance solution. These products utilize a thermally stable resin bond and selected abrasive grains, enabling them to consistently achieve a high-quality surface finish across various grinding conditions. This effectively suppresses RCF initiation and propagation, making them an ideal tool for both preventive and corrective maintenance strategies.
FAQ
What is rolling contact fatigue?
It is crack damage that starts at or just below the rail surface when cyclic contact stress exceeds the elastic limit of the steel. Microscopic plastic deformation accumulates — ratcheting — until the material toughness limit is reached and fatigue cracks form, progressing from micro-cracks through minor spalling to severe spalls that can evolve into transverse defects.
What is the difference between preventive and corrective grinding for RCF?
Preventive grinding removes an ultra-thin hardened layer, typically around 0.1 mm, on a scheduled basis so micro-defects are taken out before cracks can form. Corrective grinding is applied once RCF is detected and has to remove the crack network itself, which demands higher removal rates and full angular coverage. Both are described within the wider campaign logic in our guide to rail grinding.
What angular coverage removes RCF cracks?
On tangents and on low rails in curves, the focus is the −10° to +20° band of the rail crown. On high rails, the profile is restored to target geometry first and then ground across −10° to +45° so the fatigue damage is removed completely rather than left in the gauge corner.
What causes corrugation to develop alongside RCF?
The two often appear on the same rail because both are fed by the same contact conditions — a profile that concentrates stress in one band and a vehicle-track resonance that repeats the load. Grinding, measurement and verification of corrugation specifically are covered in rail corrugation grinding.
What happens if RCF is left untreated?
The cracks grow and link, turn into rail squat and eventually into transverse defects that threaten the rail. Spalling also degrades the surface enough to compromise ultrasonic inspection, so defects can be missed at exactly the time when detection matters most.
Get Your Customized Solution
Is your network grappling with Rolling Contact Fatigue?
Discover how the Molaton RailwayCare range of grinding wheels can empower your grinding fleet to safeguard track integrity and extend asset life with greater efficiency and lower operational costs.
Contact us now for a tailored technical proposal.
📧 Contact us: simon.wang@railwaycare.com
🌐 Explore our grinding solution: www.railwaycare.com/comm01/Rail-Grinding-Solution.htm
📱 WhatsApp: +86 15072332788